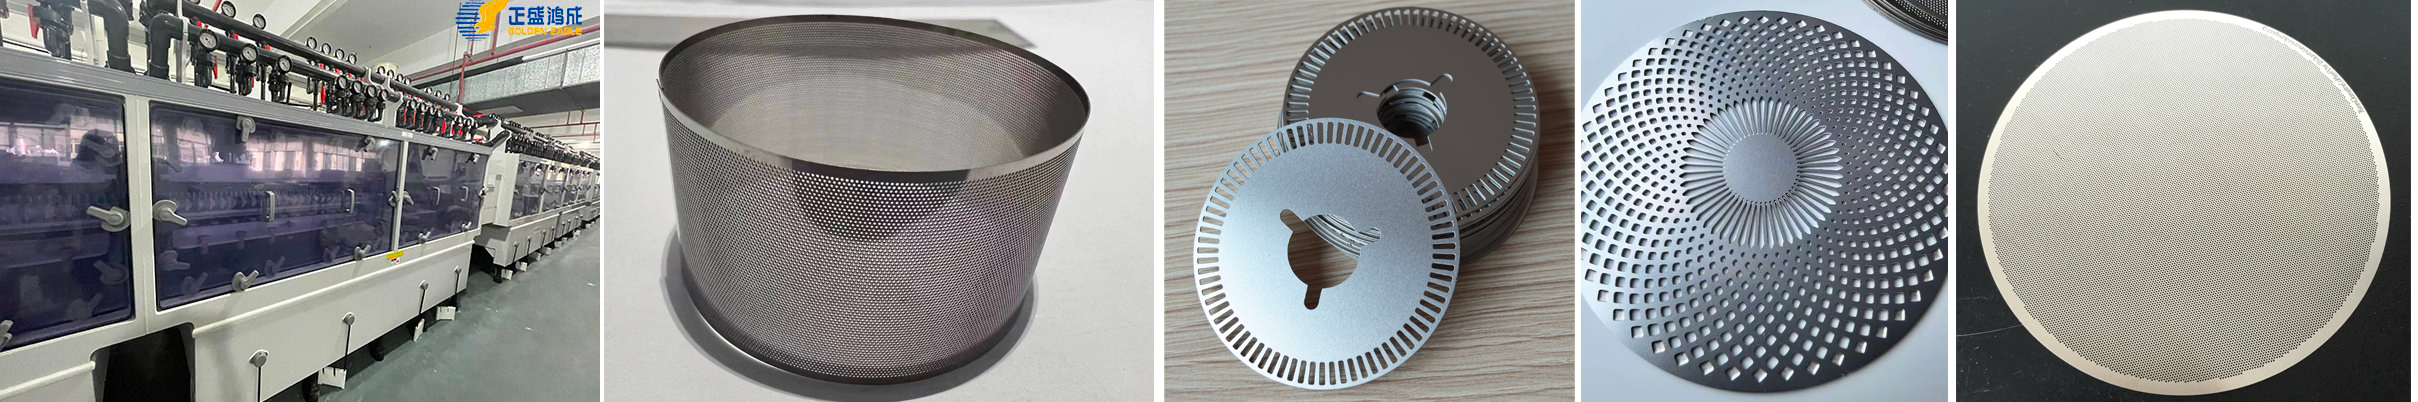
Two photoresist technologies dominate PCB etching: dry film (laminated) and liquid (sprayed or dipped). They differ on resolution, cost, throughput, and defect rate. This 2026 engineering guide compares them head-to-head and gives you a decision tree for HDI, FPC, and standard multilayer PCBs.

Dry film photoresist is factory-laminated onto copper-clad PCB panels using heated rollers, producing 25–50 µm trace resolution at the lowest cost per panel (USD 0.05/panel). Liquid photoresist is sprayed or dip-coated onto the panel and dried, achieving finer 15–25 µm resolution at higher cost (USD 0.12/panel) and is required for HDI, FPC, and any sub-50 µm work. For standard multilayer PCB (≥75 µm line/space), dry film dominates 80% of the market due to lower cost and higher throughput. Choose liquid only when you need fine-line, via-fill, or horizontal production.
Photoresist is the masking layer that protects the copper you want to keep during chemical etching. Get the resist layer wrong, and your etching machine produces scrap — under-etched shorts, over-etched opens, or lifted traces. Choosing the right photoresist technology is therefore as important as choosing the right etching chemistry.
Across our customer base (30+ countries, 500+ installed etching lines), the question of dry film vs liquid comes up in nearly every PCB quotation. Here is the full engineering comparison we use to advise customers.
Dry film photoresist is a three-layer polyester sandwich supplied on rolls:
The resist is laminated onto a clean copper panel using heated silicone rollers (110–120°C, 0.3–0.5 MPa, 1–3 m/min). After UV exposure, the unexposed resist is washed away in a sodium carbonate developer, leaving the copper circuit pattern exposed for etching.
Standard thicknesses: 25 µm (most common, 50 µm line/space), 38 µm (heavier copper, 75 µm line/space), 50 µm (thick copper, 100 µm line/space).
Liquid photoresist is a single-component or two-component negative-tone liquid applied by spin coating, dip coating, roller coating, or spray coating. The applied film is dried in an oven at 75–85°C for 15–30 minutes, then exposed and developed exactly like dry film.
Common chemistries: aqueous alkaline-developable (most common), solvent-based (declining), and direct-plate aqueous (for fine-line).
Typical dry film thickness: 5–25 µm — much thinner than dry film, which is why liquid achieves finer resolution but is more sensitive to handling.
| Parameter | Dry Film | Liquid Photoresist | Winner |
|---|---|---|---|
| Line/space resolution | 50–100 µm (25 µm resist) | 15–50 µm | Liquid |
| Cost per panel (1 m²) | USD 0.05–0.10 | USD 0.10–0.18 | Dry film |
| Throughput (m²/hour) | 30–60 (roll laminator) | 15–25 (spray + dry) | Dry film |
| Equipment cost | USD 5,000–30,000 (laminator) | USD 8,000–60,000 (coater + oven) | Dry film |
| Operator skill needed | Low (laminator is forgiving) | High (coating uniformity is critical) | Dry film |
| Edge coverage on rough copper | Poor (lifts on peaks) | Excellent (conforms to surface) | Liquid |
| Via-fill application | Not possible | Standard (electroplating, ENIG) | Liquid |
| HDI / sub-50 µm work | Not possible | Required | Liquid |
| Operator chemical exposure | None (dry rolls) | Moderate (alkaline solution) | Dry film |
| Storage & shelf life | 6–12 months (room temp) | 3–6 months (cool, dark) | Dry film |
| Compatible with horizontal conveyor etching | Excellent | Limited (liquid film can shear) | Dry film |
Use this 5-question decision tree to pick the right technology for your PCB line:
Most large PCB shops (300+ m²/day) run both technologies on parallel lines:
Both lines feed the same etching machine (e.g. GE-JM650) downstream. This is the most capital-efficient layout for 2026, and is what we recommend for any PCB shop with monthly volume above 8,000 m².
Yes — modern 25 µm dry film with optimized exposure (50–80 mJ/cm²) and a high-resolution exposure unit (4-CCD alignment, 50 µm resolution) can achieve 25 µm line/space on smooth copper. Below 25 µm, liquid photoresist is preferred because of its thinner coating and better edge acuity.
Per panel, liquid photoresist costs USD 0.10–0.18 vs USD 0.05–0.10 for dry film — roughly 2× more. The equipment is also more expensive (USD 8,000–60,000 vs USD 5,000–30,000). However, liquid achieves 15–50 µm resolution that dry film cannot, so the cost premium is justified for HDI, via-fill, and FPC.
Technically yes, but with significant delamination risk on polyimide. FPC has 25–50 µm copper bonded to 12.5–25 µm polyimide, and the substrate flexes during lamination, which lifts dry film at the edges. Liquid photoresist (sprayed) is the standard for FPC because it conforms to the polyimide surface. About 70% of FPC lines use liquid, 30% use dry film with strict tension control.
Both dry film and liquid photoresist are compatible with the three main PCB etchants: ferric chloride (FeCl₃, most common), cupric chloride (CuCl₂, regenerable, high-volume), and alkaline ammonia (best for fine-line, aluminum). The resist compatibility is in the developer (1% Na₂CO₃ for dry film; 0.85% Na₂CO₃ for liquid), not the etchant. After etching, both resists are stripped in 3–5% NaOH at 50°C.
A typical dual-roller hot-roll laminator with 600 mm working width runs at 2–3 m/min conveyor speed, equal to 80–120 m²/hour (single side) or 40–60 m²/hour (double side pass). For 24-hour continuous operation, that is 1,500–2,500 m²/day, more than enough for most multilayer PCB shops. Adding a second laminator in parallel is the typical scale-up path when production exceeds this.
If you are running dry film today and want to add liquid for HDI or via-fill, here is a step-by-step transition plan:
Whether you choose dry film or liquid photoresist, the etching machine downstream is the same. These are the platforms our customers use:
Choosing between dry film and liquid photoresist? Talk to our process engineers →